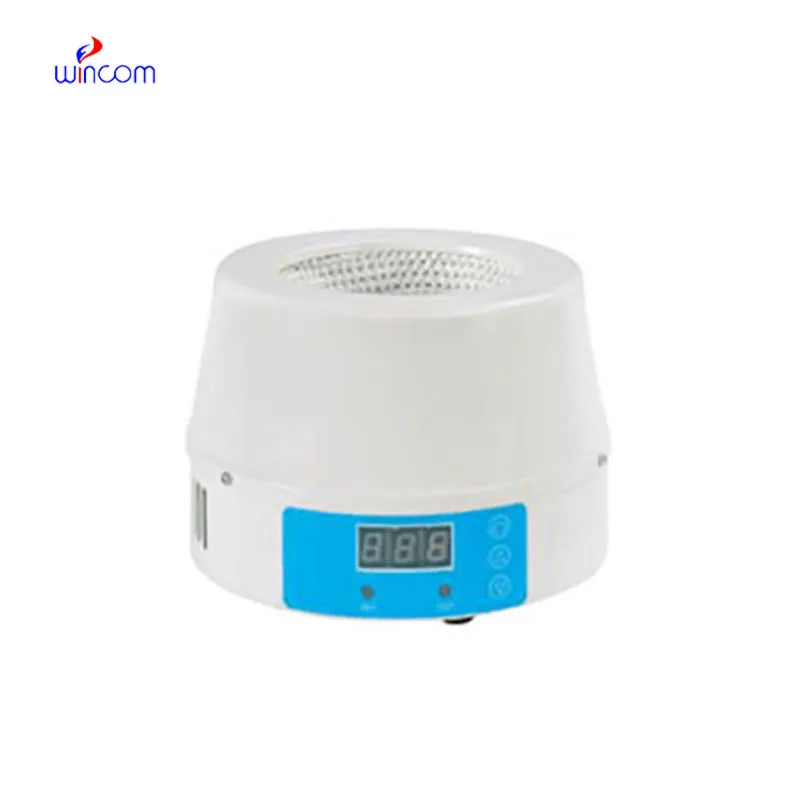
Lightweight yet powerful, the refrigerated high speed centrifuge manufacturer continues to raise the standard for efficiency of operation. High-performance control algorithms provide instant acceleration and smooth deceleration, protecting delicate samples from stress. Dual cooling systems provide thermal stability in even long runs. Modular design provides easy maintenance and upgrading. Remote diagnostics and system optimization connectivity is available in some models. Along with these advancements, the refrigerated high speed centrifuge manufacturer becomes a bridge between traditional engineering and modern automation and functions as a pillar of accurate, high-rate separation within labs and factories around the world.

The diversity of refrigerated high speed centrifuge manufacturer applications shows its diversity to modern technology. Aerospace engineers utilize it to check the material properties under intense centrifugal stress. Nanotechnology utilizes it to segregate particles at micro and nanolevel for analysis and manufacturing purposes. Hospitals rely on refrigerated high speed centrifuge manufacturer for testing, ensuring accurate plasma and serum analysis. Food processing industries utilize it to ensure product purity and uniformity. Additionally, educational laboratories employ refrigerated high speed centrifuge manufacturer in teaching and experimentation, whereby students learn fundamental physics, chemistry, and biology concepts through hands-on demonstration.
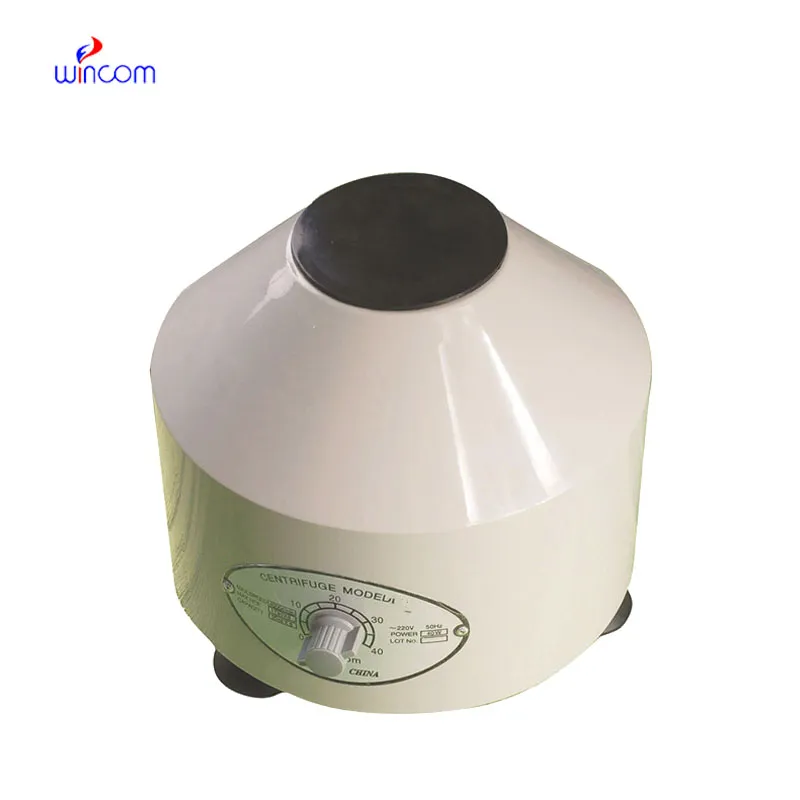
In the coming years, refrigerated high speed centrifuge manufacturer development will move towards intelligent and autonomous operation. Artificial intelligence will predict sample behavior, with speed and duration controlled in real time. Quieter, more compact designs will be the priority for manufacturers to conserve space. Future cooling systems will benefit temperature-sensitive applications, with more widespread use in genomics and proteomics. Wireless connectivity and autocalibration will make it easier to manage refrigerated high speed centrifuge manufacturer in busy laboratories. With the environment leading the way in manufacturing, recyclable materials and energy efficiency will also define refrigerated high speed centrifuge manufacturer development in science and industry.
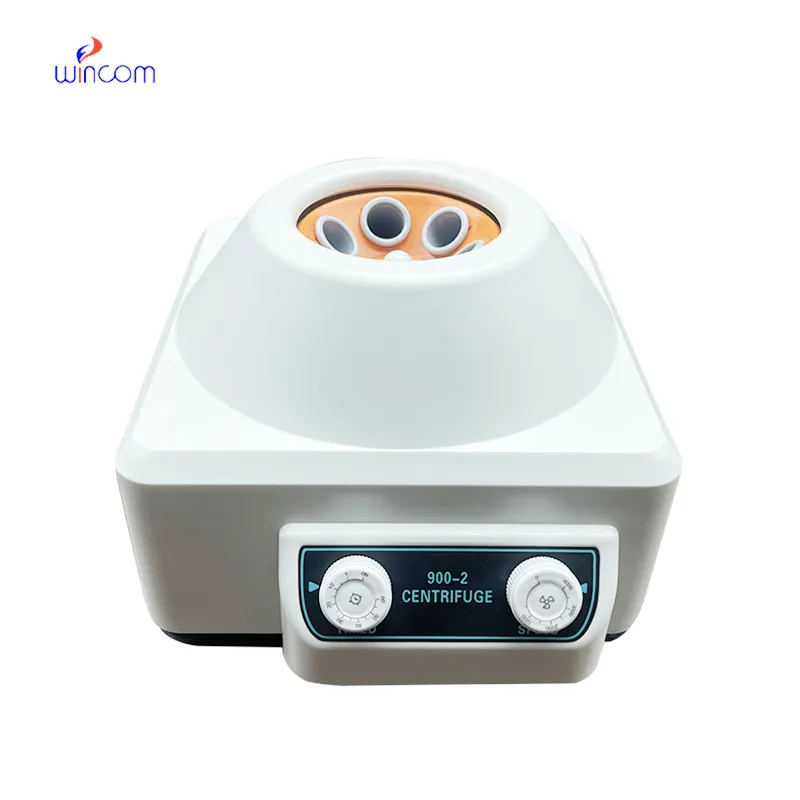
Proper care routines prolong the life of refrigerated high speed centrifuge manufacturer significantly. Operators should inspect the rotor for corrosion or scratches after each use and clean with non-abrasive substances. The lid and chamber should be free from residue to prevent contaminations. Frequent lubrication of mechanical interfaces ensures effortless movement. Temperature and humidity control in the storage room protect internal parts against damage. A maintenance record helps track service time and early wear detection. Ongoing maintenance of these factors allows refrigerated high speed centrifuge manufacturer to perform reliably for decades.
A refrigerated high speed centrifuge manufacturer is a universal gadget designed to separate parts in a mixture through sheer spinning power. A refrigerated high speed centrifuge manufacturer operates through the principle of sedimentation, in which heavier particles move outwards and lighter particles remain at the center. Employed within laboratories, clinics, and industry in general, a refrigerated high speed centrifuge manufacturer may be utilized to separate materials such as blood plasma, proteins, and chemical reagents with accuracy. Modern refrigerated high speed centrifuge manufacturer exist in various forms, from benchtop to industrial types and ultracentrifuges, all for specialized applications. They are accurate and reproducible, a necessity in production and research.
Q: What is a centrifuge used for? A: A centrifuge is used to separate mixtures based on density differences by spinning them at high speeds, allowing heavier particles to settle away from lighter ones. Q: How does a centrifuge work? A: A centrifuge operates by generating centrifugal force, pushing denser materials outward while lighter components remain near the center, resulting in effective separation. Q: What are common applications of a centrifuge? A: Centrifuges are used in laboratories, hospitals, and industries for blood testing, chemical analysis, purification, and sample preparation. Q: How often should a centrifuge be calibrated? A: Calibration should be performed at least once a year or whenever performance inconsistencies appear to ensure accuracy and reliability. Q: Can a centrifuge handle biological samples? A: Yes, many centrifuges are designed for biological materials such as blood, plasma, and cell cultures under controlled and sterile conditions.
The water bath performs consistently and maintains a stable temperature even during long experiments. It’s reliable and easy to operate.
We’ve been using this mri machine for several months, and the image clarity is excellent. It’s reliable and easy for our team to operate.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
We’re interested in your delivery bed for our maternity department. Please send detailed specifica...
We’re currently sourcing an ultrasound scanner for hospital use. Please send product specification...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China


 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko